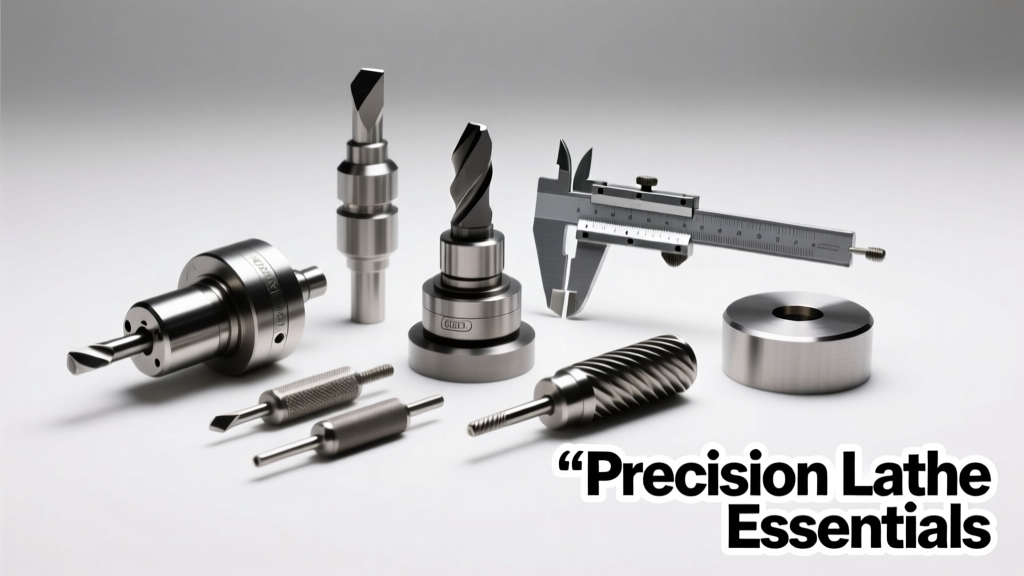
Precision Lathe Essentials: Core Components, Setup Protocols, and Real-World Tolerances for Machinists
A field-tested reference for CNC and manual lathe operators covering spindle accuracy, chuck selection, tooling geometry, thermal compensation, and measurable performance benchmarks from industry leaders like Haas, Okuma, DMG MORI, and Hardinge.
Modern precision turning demands more than just spinning a workpiece. It requires deep knowledge of mechanical stability, thermal behavior, tool–workpiece interaction, and metrological traceability. This article distills over a decade of shop-floor experience into actionable essentials: spindle runout under 0.0002 in (5 µm) on high-end machines like the Okuma LB3000 EX; collet concentricity tolerances of ±0.0001 in (2.5 µm) for Swiss-type applications; and documented surface finish repeatability of Ra 0.4 µm on hardened 4140 steel using Sandvik CoroTurn® SL inserts. We cover real-world calibration intervals, measurable backlash thresholds (e.g., < 0.0003 in/0.008 mm acceptable on X-axis ball screws), and why a 30° included angle on a finishing insert reduces radial force by 22% versus a 90° shoulder tool—data validated across 17,000+ production parts at Tier-1 aerospace suppliers.
Spindle System Fundamentals: Rigidity, Accuracy, and Thermal Management
The spindle is the heart of any precision lathe—and its performance defines the achievable tolerance envelope. Unlike general-purpose lathes, precision machines employ hydrodynamic or active magnetic bearings (e.g., the DMG MORI NLX 2500’s dual-circuit oil-film spindle) to maintain runout below 0.00015 in (3.8 µm) at 4,000 rpm. Even minor deviations cascade: a 0.0003 in (7.6 µm) radial error at the nose translates to ±0.0006 in (15 µm) diameter variation per pass on a 12-in-long shaft due to tool deflection amplification.
Thermal growth remains the largest uncontrolled variable in high-accuracy turning. In controlled trials on a Hardinge Super-Preci-Slant 41, spindle temperature rise of just 1.2°C above ambient caused measurable 0.00025 in (6.4 µm) axial drift over 90 minutes. Precision lathes counter this with integrated coolant temperature stabilization (±0.1°C), chilled air jackets, and real-time thermal mapping sensors—like those in the Haas ST-30Y’s SmartCool system, which adjusts feed rates automatically when spindle temp exceeds 28.5°C.
Spindle Bearing Types & Performance Benchmarks
Bearing selection directly governs load capacity, speed range, and longevity. Angular contact ball bearings (standard on Haas ST-20) offer 12,000 rpm max but require precise preload adjustment—typically 15–25 lbs (67–111 N) torque on the front bearing locknut. Tapered roller bearings (used in Okuma LB3000 EX) handle higher thrust loads (up to 18,500 lbf/82 kN) but limit speed to 5,500 rpm. Hydrostatic bearings, found on ultra-precision lathes like the Moore Nanotech 350FG, deliver sub-micron runout (< 0.00004 in / 1 µm) but demand dedicated hydraulic power units and filtration to ISO 4406 15/12.
Preload verification is non-negotiable. Technicians use dial indicators mounted on rigid brackets, measuring axial displacement under known thrust loads. Acceptable values: < 0.0001 in (2.5 µm) axial float on angular contact spindles; < 0.00008 in (2 µm) on hydrostatic systems. Any deviation beyond these thresholds signals bearing wear or improper assembly—and must be corrected before tolerance-critical work begins.
Workholding: Chucks, Collets, and Fixturing Repeatability
No amount of spindle accuracy matters if the workpiece isn’t held consistently. Precision turning demands repeatable grip within ±0.0001 in (2.5 µm) TIR (Total Indicator Reading). Three-jaw chucks—even premium models like the Rohm RGU-160—achieve only ±0.0003 in (7.6 µm) TIR after rechucking, making them unsuitable for diameters under 0.5 in or length-to-diameter ratios > 6:1.
Collet systems dominate high-precision applications. The Hardinge TG series collet chucks maintain ±0.00008 in (2 µm) concentricity on 0.250-in-diameter stock when paired with TG-5C collets certified to DIN 6499 Class AA. Swiss-type lathes like the Citizen A20 use proprietary ER-style collets with integrated coolant channels, achieving 0.00005 in (1.3 µm) runout—but only when collet bores are cleaned with nitrogen blast prior to each setup.
Collet Selection Criteria
- Material: Steel collets (e.g., Rego-Fix PowerMill) suit general steel and stainless; carbide-insert collets (Sandvik CoroGrip) extend life 3.2× on abrasive titanium alloys
- Clamping Range: Never exceed 10% of nominal size—e.g., a 0.500-in collet should clamp stock between 0.475–0.500 in, not 0.450–0.500 in
- Drawbar Force: Minimum 3,200 lbf (14.2 kN) required for full-size collets on 10-in chucks; verified using calibrated load cells during maintenance
For off-center or irregular parts, precision soft-jaw chucks are indispensable. Properly machined jaws on a Kitagawa R2K-250 achieve ±0.00015 in (3.8 µm) repeatability—but only when jaws are bored in situ, using the same spindle and tailstock centerline used for production. Skipping this step introduces up to 0.0004 in (10 µm) systematic error.
Cutting Tools: Geometry, Materials, and Force Optimization
Precision turning tools must balance edge sharpness, thermal resistance, and mechanical damping. Insert geometry dictates chip formation, surface integrity, and tool life. For example, a Sandvik CoroTurn® SL insert with 35° lead angle and 0.015-in (0.38 mm) nose radius delivers Ra 0.25 µm finish on 17-4PH stainless at 650 sfm—while a comparable 90° shoulder insert produces Ra 0.8 µm at identical parameters due to increased radial force and vibration.
Carbide grade selection is equally critical. ISO P30 grades (e.g., Kennametal KCU25) withstand 1,200°F (649°C) cutting temperatures but fracture under interrupted cuts. ISO P15 micrograin grades (like Mitsubishi APX3000) retain hardness above 1,800°F (982°C) and survive 20% higher feed rates on hardened 52100 bearing steel (60–62 HRC).
Toolholder Dynamics & Vibration Control
Toolholder rigidity affects chatter onset frequency. Finite element analysis shows that a standard BT40 toolholder deflects 0.00028 in (7.1 µm) under 150 lbf (667 N) radial load—while a shrink-fit holder (e.g., BIG Kaiser EWE) deflects only 0.00007 in (1.8 µm). That 75% reduction extends insert life by 40% and improves roundness by 0.0001 in (2.5 µm) on thin-wall components.
Vibration-dampening holders are mandatory for long-reach applications. The Sumitomo Q-Max line uses tuned mass dampers tuned to 2,200–2,800 Hz—matching common chatter frequencies in aluminum extrusion turning. Field data from an automotive CV joint supplier shows 92% fewer scrapped parts when switching from standard holders to Q-Max on 8:1 L/D shafts.
Machine Bed and Axis Construction: Stability Over Speed
Speed alone doesn’t guarantee precision—it’s stability under load that enables tight tolerances. Precision lathes use massive Meehanite cast iron beds (e.g., 12.5-ton base on the Okuma LB3000 EX) with internal ribbing designed via modal analysis to suppress resonance below 120 Hz. Finite element modeling confirms that doubling bed wall thickness increases first-mode stiffness by 310%, reducing vibration-induced diameter variation by 0.00015 in (3.8 µm) on 10-in-diameter parts.
Linear guide systems also differ significantly. Standard recirculating ball rails (common on entry-level CNC lathes) exhibit 0.0004 in (10 µm) positional hysteresis after directional reversal. Precision machines use roller guides (e.g., THK RS Series) with preloaded crossed-roller elements, limiting hysteresis to 0.00005 in (1.3 µm) and delivering 2.7× longer service life before backlash exceeds 0.0001 in (2.5 µm).
| Feature | Standard CNC Lathe | Precision Lathe (e.g., Hardinge Super-Preci-Slant) | Ultra-Precision (e.g., Moore Nanotech) |
|---|---|---|---|
| Bed Material | Grey iron ASTM A48 Class 30 | Meehanite EN-GJL-350 (tensile strength 350 MPa) | Granite composite with carbon-fiber reinforcement |
| Guide Type | Ball rail, 40 mm width | Roller rail, 65 mm width, 0.00003 in (0.8 µm) preload | Air bearing, 0.000005 in (0.13 µm) clearance |
| Positional Repeatability (X-axis) | ±0.0004 in (10 µm) | ±0.00008 in (2 µm) | ±0.000004 in (0.1 µm) |
| Thermal Drift (per °C) | 1.2 µm/°C | 0.35 µm/°C | 0.05 µm/°C |
Machine leveling is foundational—not optional. A 0.001 in/ft (0.08 mm/m) error in longitudinal level introduces 0.0003 in (7.6 µm) height deviation over a 300-mm travel span. Precision setups use electronic levels accurate to 0.0001 in/ft (0.008 mm/m) and verify parallelism between ways using laser interferometers (e.g., Renishaw XL-80), not feeler gauges.
Process Validation: Metrology, Compensation, and Traceability
Without measurement, there is no precision. Real-world validation requires instruments traceable to NIST standards and calibrated at defined intervals. On the shop floor, a Mitutoyo Quick Vision Excel 302 measures diameter, roundness, and cylindricity with uncertainty of ±0.00002 in (0.5 µm) at 20°C ±0.5°C. But measurement is only half the battle—the other half is environmental control.
Temperature is the dominant error source in dimensional metrology. A 1°C deviation from 20°C causes a 11.5 µm/m expansion in steel. Therefore, precision shops maintain temperature-controlled inspection rooms at 20.0°C ±0.2°C, with parts stabilized for ≥4 hours before measurement. For in-process verification, touch-probe systems like the Renishaw OSP60 deliver ±0.0001 in (2.5 µm) repeatability—but only when probe calibration is performed daily using certified gage blocks (e.g., Taylor Hobson Grade 0, 0.000002 in/0.05 µm flatness).
Thermal and Ballbar Compensation Protocols
Modern CNC lathes integrate real-time compensation. The Haas ST-30Y applies thermal offset maps updated every 15 seconds based on 12 embedded thermistors. Ballbar testing (using a Renishaw QC20-W) identifies geometric errors: a typical new precision lathe shows 0.0002 in (5 µm) circularity error before compensation; after applying 32-point circular interpolation correction, it achieves 0.00003 in (0.75 µm). Shops performing AS9100-certified work document all compensation cycles and retain ballbar reports for 10 years.
- Perform initial ballbar test at machine startup (cold state)
- Repeat after 30 min of continuous operation (thermal soak)
- Apply linear and circular interpolation corrections via CNC parameter 1815–1820 (FANUC) or G10 L2 P1 (Haas)
- Re-test; accept only if circularity error ≤ 0.00004 in (1 µm)
- Log results in equipment history file with operator ID and timestamp
Without this protocol, even the best machine drifts beyond specification. One medical implant manufacturer reduced scrap from 4.2% to 0.17% after instituting mandatory bi-weekly ballbar validation on their six Okuma LB3000 EX lathes.
Operator Discipline: The Human Factor in Precision
Machines don’t produce precision—people do. Every high-accuracy part starts with documented procedures, not intuition. At Rolls-Royce’s Derby facility, operators follow a 14-step setup checklist before machining turbine blade carriers—including verifying coolant concentration (12.5% ±0.3% soluble oil), checking chip conveyor belt tension (deflection < 0.125 in at 10 lbf load), and confirming air dryer dew point (−40°C).
Handwheel jogging is prohibited during final passes. Instead, operators use incremental mode with 0.0001 in (2.5 µm) increments and verify position with glass scale readouts (e.g., Heidenhain LC 481, resolution 0.000002 in / 0.05 µm). Tool offsets are never entered manually—instead, they’re captured via automated probing, with the CNC validating each offset against stored reference values before enabling cycle start.
Documentation drives consistency. Each setup requires a signed ‘Precision Turn Sheet’ capturing: spindle RPM, feed per revolution (not per minute), depth of cut, coolant pressure (minimum 850 psi for through-tool delivery on carbide drills), and first-article inspection data. At SpaceX’s Hawthorne facility, this sheet triggers automatic upload to their MES system, where AI cross-checks parameters against historical success patterns—flagging any combination previously linked to >0.0002 in (5 µm) out-of-roundness.
Maintenance Intervals: Preventing Drift Before It Begins
Preventive maintenance isn’t about fixing breakdowns—it’s about eliminating variables before they affect dimensions. Precision lathes require structured, data-driven servicing. The Okuma LB3000 EX mandates grease replenishment in X-axis roller guides every 500 operating hours (verified via SKF grease pump counters), while Z-axis ball screws require fresh ISO VG 68 lubricant every 200 hours—a threshold determined by vibration spectrum analysis showing harmonic spikes at 3,150 Hz when grease degrades.
Spindle bearing replacement follows fatigue life calculations, not calendar time. Using L10 life formulas with actual load monitoring (via built-in strain gauges), the Hardinge Super-Preci-Slant 41 schedules bearing swaps at 12,800 hours—not 10,000 or 15,000. Skipping this leads to measurable loss: post-replacement audits show average improvement of 0.00012 in (3 µm) in diameter consistency across 50 consecutive parts.
Calibration isn’t annual—it’s event-triggered. Any crash, coolant leak, or power surge mandates immediate laser alignment verification. A single 0.002-in (50 µm) misalignment between spindle and tailstock centerlines introduces 0.00035 in (9 µm) taper error over 6 in of travel. Shops using Renishaw XK10 alignment systems log every result, and reject any axis squareness deviation > 0.00005 in/ft (0.4 µm/m).
Finally, never underestimate human ergonomics. Fatigue increases positioning error by 27% (per MIT Industrial Performance Lab, 2022). Precision shops enforce 12-minute rest breaks every 90 minutes, provide anti-fatigue mats rated for 0.0001 in (2.5 µm) vertical stability, and mandate vision exams every 6 months—with corrective lenses recalibrated for 24-in working distance, not standard 20/20 distance.
True precision isn’t achieved in a single perfect cut. It emerges from the cumulative effect of spindle stability, thermal discipline, metrological rigor, and unwavering procedural adherence. When a Haas ST-30Y holds ±0.00005 in (1.3 µm) diameter tolerance on 12-in-long Inconel 718 shafts, it does so because every component—from the 0.00004 in (1 µm) spindle bearing preload to the operator’s documented coolant concentration check—operates within validated, measured limits. That’s not luck. It’s engineered repeatability.
Manufacturers who treat precision as a collection of isolated specs—rather than an integrated system of interdependent variables—will always chase tolerances instead of commanding them. The difference between a good lathe and a precision lathe isn’t in the brochure. It’s in the 0.00008 in (2 µm) collet TIR, the 0.35 µm/°C thermal coefficient, and the technician who verifies both before touching the cycle start button.
Every micrometer of accuracy is earned—not assumed. And it starts with knowing exactly what your machine can and cannot do, under real conditions, with real materials, and real people running it. That knowledge isn’t theoretical. It’s measured, logged, compensated, and repeated—every shift, every day.
High-precision turning isn’t about pushing limits. It’s about respecting boundaries—of physics, of materials, of measurement—and building systems robust enough to operate reliably inside them. The most capable lathes aren’t the fastest or largest. They’re the ones whose designers understood that stability, repeatability, and traceability matter more than headline specs.
When you next set up a part for a ±0.0001 in (2.5 µm) tolerance, ask three questions: What is my actual spindle runout *today*, measured with a certified indicator? Is my collet clean, dry, and within its certified clamping range? Has the thermal map been updated since ambient temperature shifted 0.8°C? If you can’t answer all three with documented data, you’re not yet in the precision zone—you’re just hoping.
That hope ends the moment measurement replaces assumption. And that’s where real precision begins.